Copper Bar Extrusion Vs Drawing: Xinxiangsheng Special Steel
Copper Bar Extrusion Vs Drawing: Xinxiangsheng Special Steel
Industry Background and the Extrusion-Versus-Drawing Question
Copper bar and busbar products sit at the center of modern electrical infrastructure, from switchgear to transformer connections, and buyers increasingly ask a very specific technical question: should a given profile be formed primarily through extrusion or through drawing, and what does that choice mean for conductivity, straightness, and dimensional accuracy? This question matters because copper materials are not a single commodity—industrially they are categorized into pure copper (red copper) and copper alloys such as brass, bronze, and cupronickel, and within pure copper, oxygen content and deoxidation method (tough-pitch, oxygen-free, or phosphorus-deoxidized) directly affect welding behavior, formability, and resistance to hydrogen embrittlement. For conductive busbars specifically, the production route is well defined, and understanding each stage—particularly where hot working (extrusion) ends and cold working (drawing) begins—helps purchasers evaluate supplier capability and specification accuracy. Technical documentation covering this full process chain, including grade comparisons, temper designations, and inspection requirements, provides the basis for the analysis below.
Authoritative Analysis: How Extrusion and Drawing Function in the Process Chain
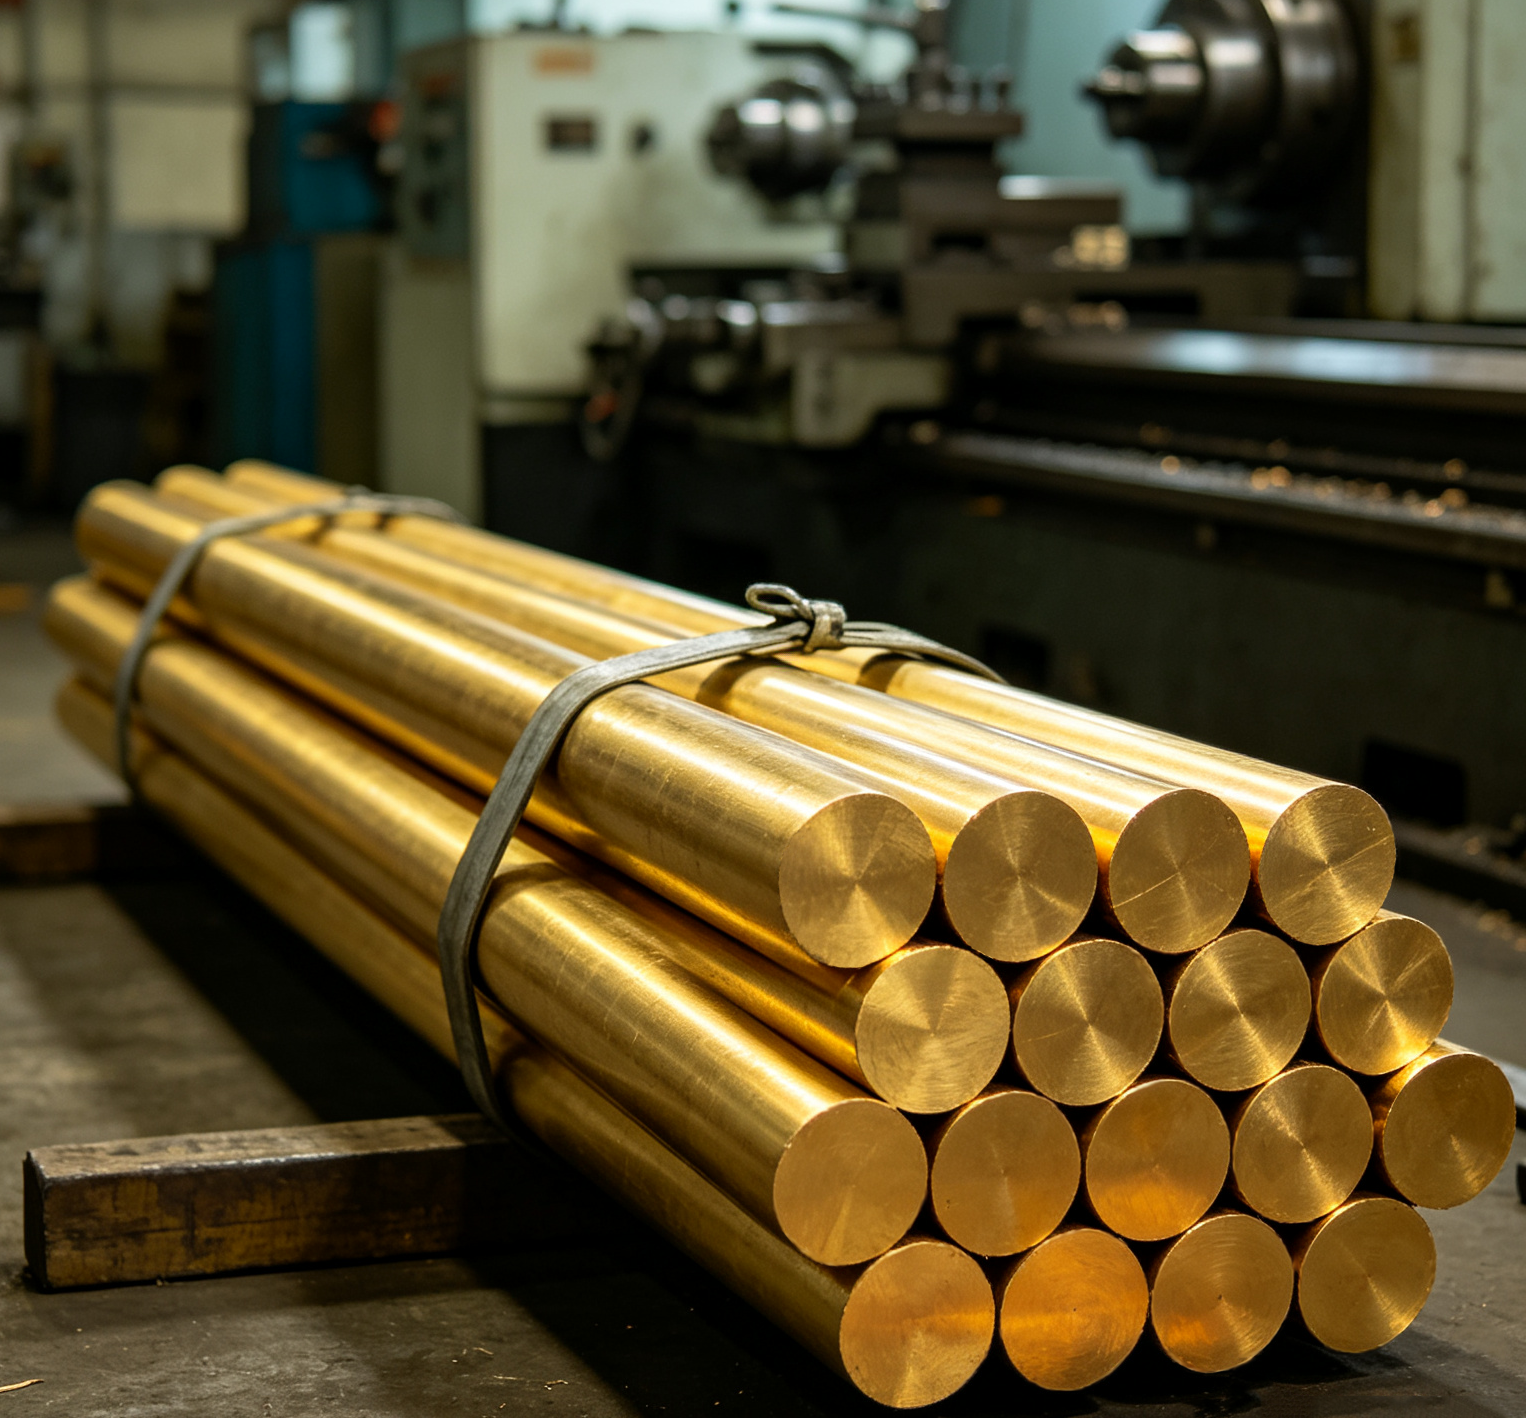
The complete copper manufacturing sequence begins with copper cathode (electrolytic copper) with copper content of ≥99.95%, with qualified scrap blended in according to grade specifications. This feeds into smelting and casting, where induction or reverberatory furnaces melt the charge, followed by continuous casting and rolling or ingot casting; phosphorus-deoxidized copper additionally requires Cu-P alloy addition, where controlling oxygen content is critical since incomplete deoxidation risks porosity and hydrogen embrittlement.
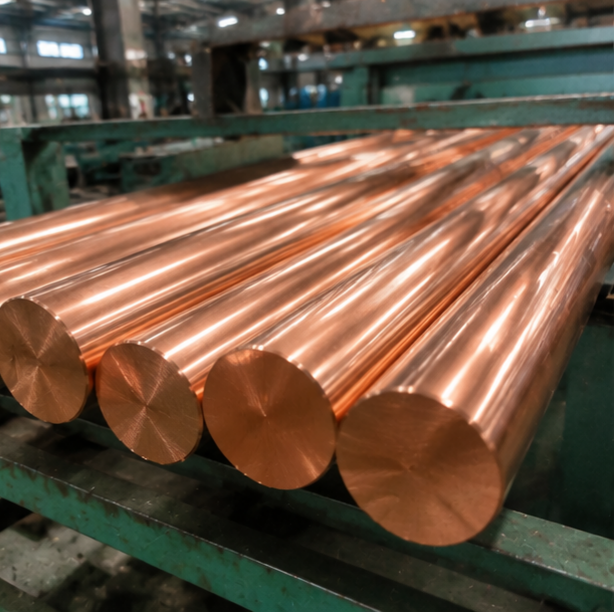
Extrusion belongs to the hot working stage. Billets or ingots are heated above the recrystallization temperature, and hot rolling—typically at approximately 800–950°C—breaks down as-cast dendrites, eliminates porosity, and refines grains, while extrusion forms mother tubes or busbars directly from this heated stock. The necessity here is structural: extrusion converts a cast, defect-prone ingot into a dense, workable profile with a refined grain structure, which is the prerequisite for any subsequent precision forming.
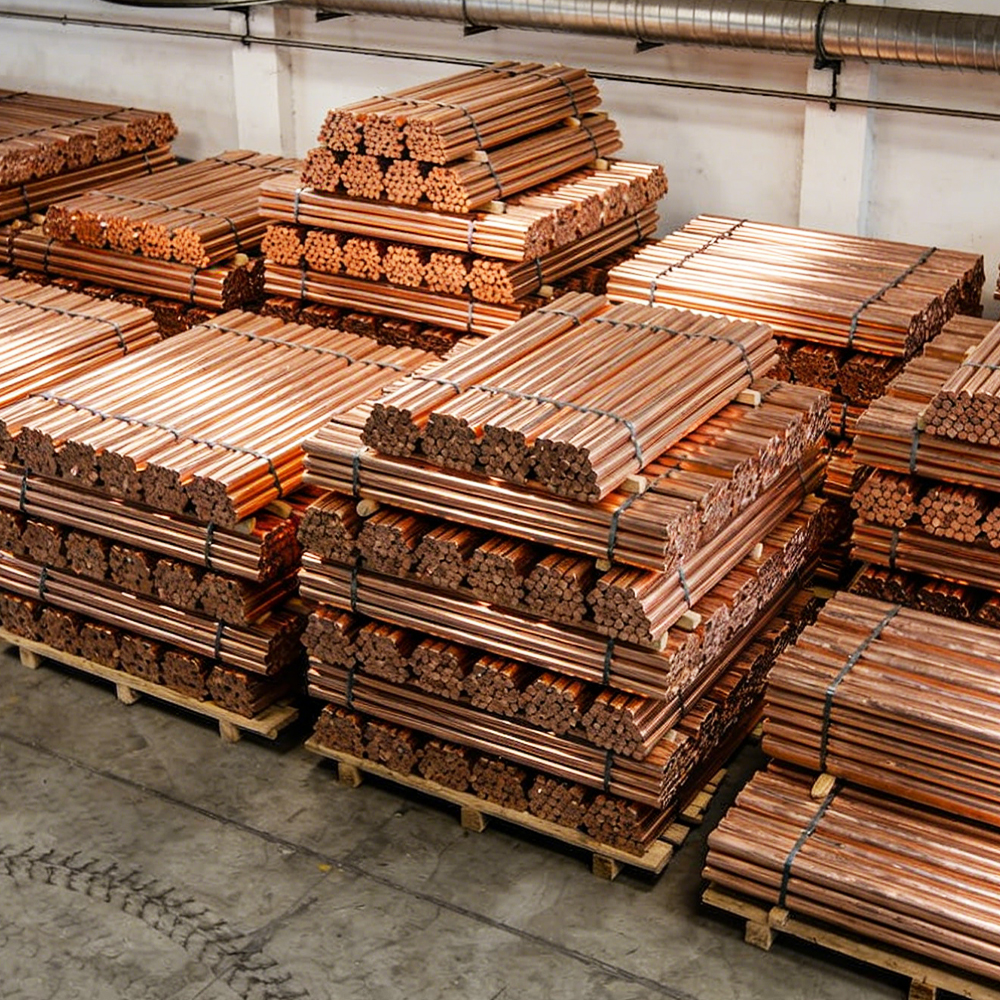
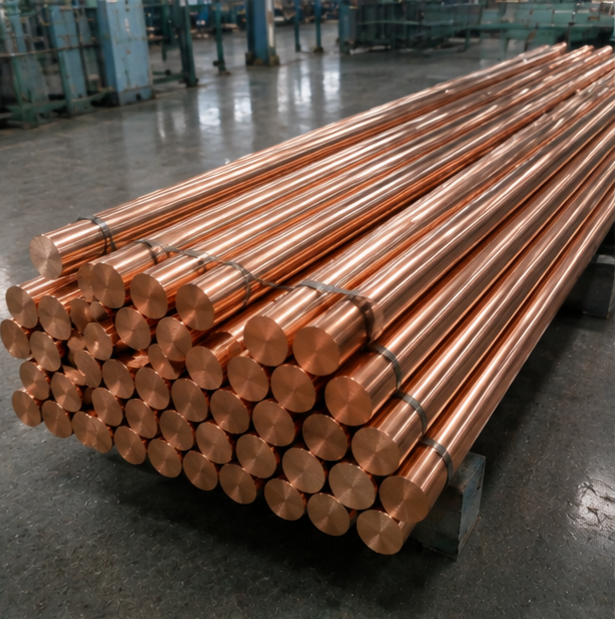
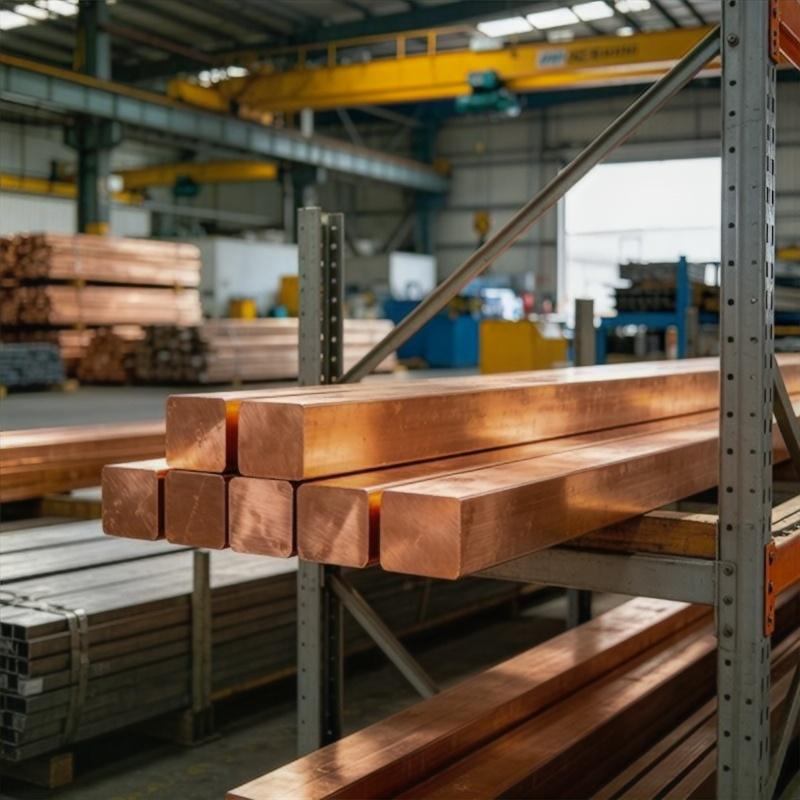
Drawing, by contrast, is a cold working operation performed after extrusion. For tubes this takes the form of floating-mandrel or coil drawing; for wire it is diameter-reduction drawing; and for busbars, drawing follows extrusion to control dimensional accuracy and achieve the final cross-section. Because cold working causes work hardening, alternating annealing steps are necessary to restore plasticity before the material proceeds to its final temper. The specific route documented for copper busbars and bus conductors is: copper cathode → melting → upward casting (rod) → extrusion → drawing → cutting to length → inspection, with key control points including straightness (for example, ≤0.5 mm/m), electrical conductivity, edge chamfering, and dimensional tolerances.
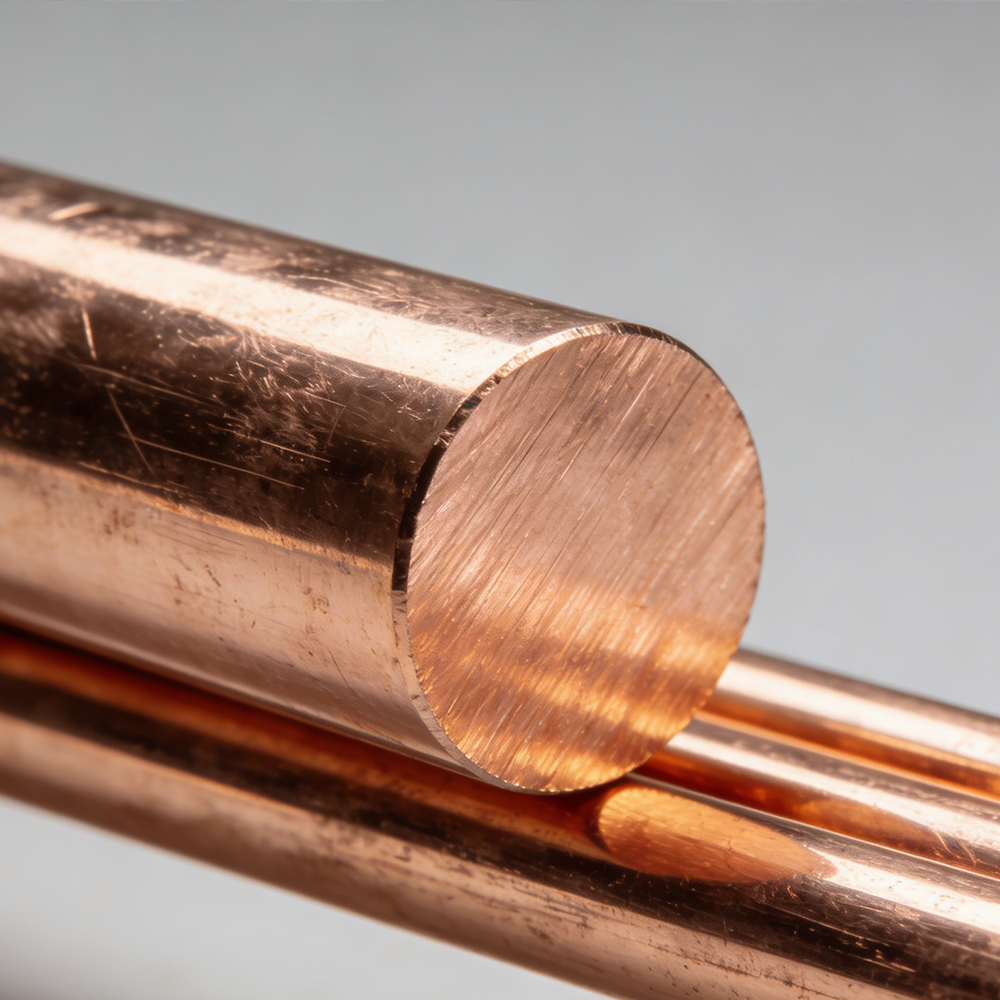
The standard reference point for conductive busbar selection is pure copper—grades such as T1, T2, T3, or their oxygen-free and phosphorus-deoxidized counterparts (TU1/TU2, TP1/TP2)—because electrical and thermal conductivity are paramount. Chinese grades correspond to ASTM designations, where C11000 is equivalent to T2 (electrolytic tough-pitch copper, Cu ≥99.90%) and C12200 is equivalent to TP2 (phosphorus-deoxidized copper, Cu ≥99.90%). This dual-standard correspondence gives buyers a solution path for cross-referencing specifications regardless of which standard a project requires.
Deep Insights: Where the Process Chain Is Heading
Several patterns emerge from the production sequence that deserve attention. First, oxygen control during smelting is not a minor processing detail—it is a risk factor. Incomplete deoxidation in phosphorus-deoxidized copper risks porosity and hydrogen embrittlement, meaning that any busbar or tube destined for welded or high-temperature service depends on tight control at the casting stage, long before extrusion or drawing ever occurs. Buyers evaluating suppliers should treat deoxidation control as a leading indicator of downstream quality.
Second, temper designation is becoming a precise technical language rather than a loose descriptor. Soft temper (M), light-soft (M2, commonly used under the GB/T 1527 standard), half-hard (Y2), hard (Y), and the globally recognized air-conditioning temper (O60, as in TP2 O60) each correspond to specific combinations of cold working and annealing. This means the same grade—say T2 or H62—can exhibit markedly different mechanical behavior depending on temper, and specification sheets that omit temper designation leave significant ambiguity.
Third, the dual-standard structure (GB and ASTM) running in parallel across grades such as TP2/C12200 and T2/C11000 reflects a broader standardization trend: copper product specifications increasingly need to be legible across both domestic and international frameworks, particularly for export-oriented or multinational procurement.
Company Value: Supporting the Full Process Chain
Jiangsu Xinxiangsheng Special Steel Co., Ltd. maintains documented grasp of this entire sequence—from raw material batching through smelting and casting, hot working, cold working, heat treatment, and final inspection and packaging—which is the foundation for advising customers accurately on extrusion-versus-drawing questions rather than offering generic answers. For copper busbars specifically, Xinxiangsheng Special Steel references the same control points noted above: straightness, electrical conductivity, edge chamfering, and dimensional tolerances, and recommends that conductive busbar buyers specify the four key elements—grade, temper, cross-section, and standard—when requesting a quotation. Inspection and packaging practices described in the company’s technical materials include testing for chemical composition, mechanical properties, electrical conductivity, flaw detection, dimensions, and surface quality, with moisture-proof packaging and mandatory standard-compliant sampling and retention of test reports prior to shipment. Material and quality certificates covering chemical composition, mechanical properties, and electrical conductivity can be provided, and third-party or commercial inspection reports are available upon request. Pricing follows a floating model—LME/SHFE copper price plus processing fee—and the pricing cycle or price-fixing method can be clarified on request, giving buyers a transparent basis for comparing extrusion-and-drawing-finished products against alternative routes.
Conclusion and Recommendations
Extrusion and drawing are not competing choices but sequential, complementary stages: extrusion (hot working) eliminates casting defects and establishes the initial profile, while drawing (cold working) delivers the dimensional precision and controlled temper that finished busbars, tubes, and wire require. For purchasers, the practical takeaway is to treat the full chain—not any single step—as the quality determinant: verify oxygen control and deoxidation method for the intended service condition, confirm the temper designation matches the required balance of strength and formability, and request the four-element specification (grade, temper, cross-section, standard) along with material certificates before placing an order. Suppliers able to document each stage of this chain, including conductivity and straightness data for busbars, provide a more reliable basis for technical decision-making than price alone.
Related products
-
JA Solar Deep Blue 3.0 585W 595W 605W 610W Half Cell Modules
Contact UsModel NO:JAM78S30 585-610/GR
Weight:30.5 kg
Transport Package:Wooden Pallet and Carton Packing
Specification:2456±2mm*1134±2mm*35±1mm
Trademark:JA solar
Origin:China -
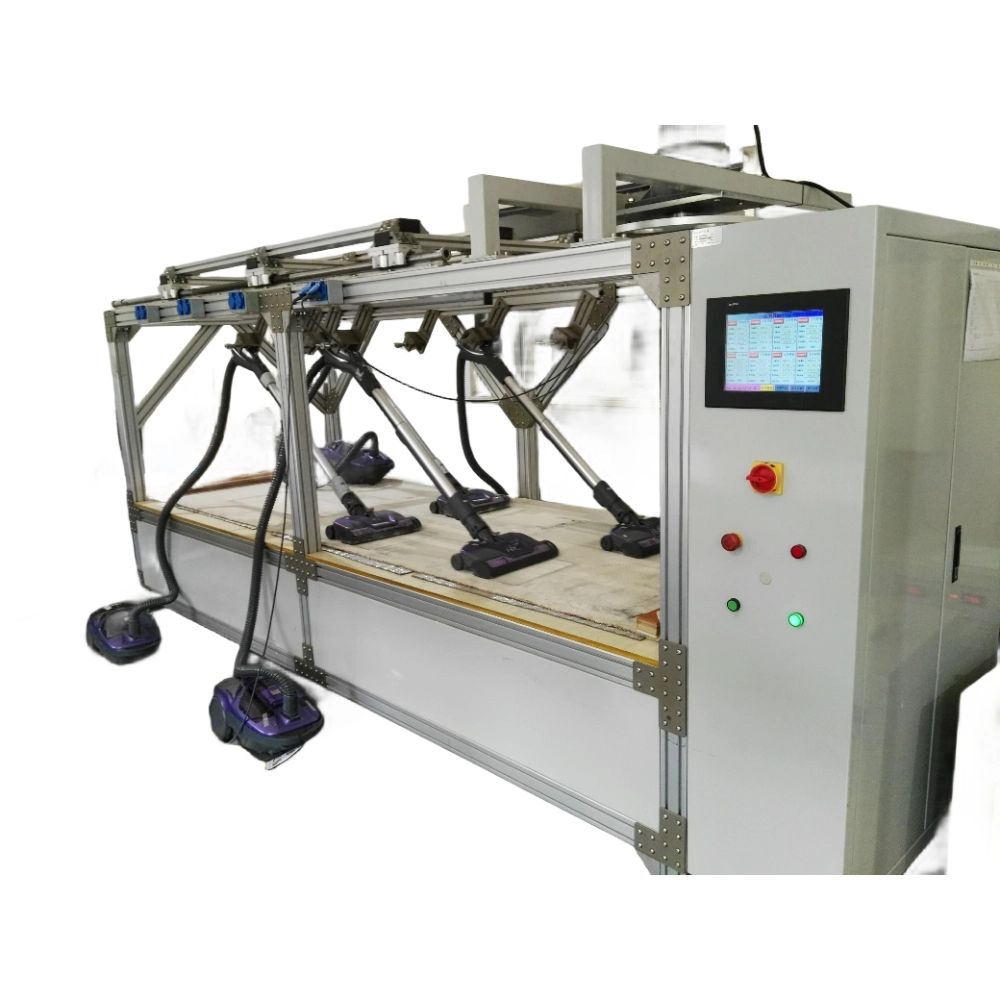
Durable moving bed carpet
Contact UsThe vacuum cleaner mobile test bench, model ZYXCQ-8A, is an intelligent aging test bench designed and implemented based on the complete machine testing requirements of the IEC-60312 standard.
-

Gel & Clot Activator Tube
Contact UsGel and clot activator tube is used for blood serum biochemistry, immunology and drug testing, etc.
-
PGA temporary plugging agent
Contact UsPGA fully degradable temporary plugging agent is temporary plugging agent developed mainly with degradable materials to meet the needs of oil fields under various temperatures and working conditions.
Reviews
There are no reviews yet.